01
Agree the basis
Control narrative, I/O list and HMI requirements are agreed before coding starts.
WETS AI writes PLC and HMI programs in-house for Allen-Bradley, Siemens and Schneider Electric control systems. Each program is written from the agreed control narrative, loaded into your panel in our Houston shop, tested at the factory acceptance test before anything ships, and checked again on site at SAT.
We program the three platforms most used in Texas plants. We confirm the exact controller and software version with you before programming starts.
| Brand | Typical controllers | Programming software |
|---|---|---|
| Allen-Bradley (Rockwell Automation) | Micro800, CompactLogix, ControlLogix | Connected Components Workbench (CCW), Studio 5000 Logix Designer |
| Siemens | SIMATIC S7-1200, S7-1500 | TIA Portal |
| Schneider Electric | Modicon M340, M580 | EcoStruxure Control Expert |
Allen-Bradley, Siemens and Schneider Electric are trademarks of their respective owners. WETS AI is not affiliated with these companies.
The PLC sits at the centre. The HMI, remote I/O and drives all talk to it over one industrial Ethernet network.
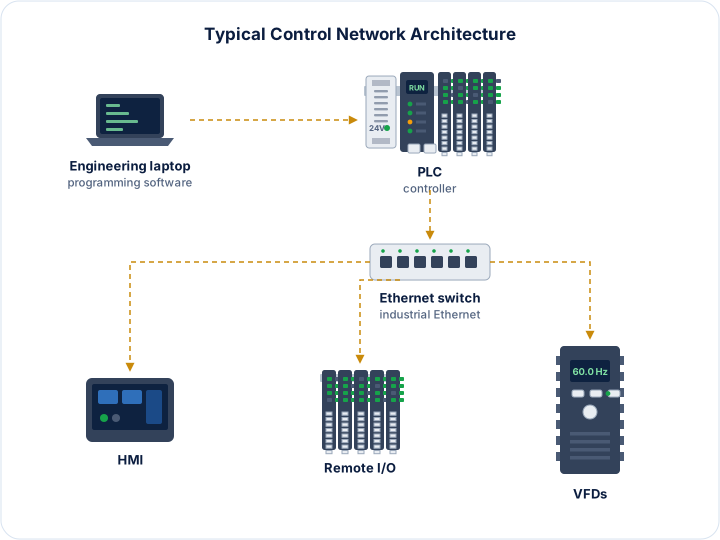

The PLC program carries out the control narrative. The HMI gives operators a clear view of the process and the right controls for their role.
Control narrative, I/O list and HMI requirements are agreed before coding starts.
The program is written and checked internally against the narrative.
Every I/O point is simulated and the sequences, alarms and interlocks are tested with the panel.
On site, the program is checked again with the real instruments and equipment.
A program is only useful if the people who own it can understand it years later. We use consistent tag names, comments on every routine, and a clear structure that follows the sections of the control narrative.
If your company has a programming standard, we follow it. At handover you receive the final program files and backups along with the rest of the panel documentation.

When the system is accepted, you get everything your team needs to run and support it without calling us for every change.
We also update existing programs when a plant moves to a newer controller, for example from an older Allen-Bradley or Siemens platform, keeping the sequences your operators already know.
Both. We can write the program from your control narrative, or load and test a program your team has written.
Yes. At the factory acceptance test the PLC and HMI are loaded with the final program, every I/O point is simulated, and alarms, interlocks and sequences are tested.
Yes. Send us your standard and we will follow its structure, naming and screen conventions.
Yes. We can modify existing Allen-Bradley, Siemens and Schneider Electric programs, including when a system moves to a newer controller.
Common industrial networks such as EtherNet/IP, PROFINET and Modbus TCP, depending on the platform and the devices in your system.
Control narratives, HAZOP and SIL identification, process flow diagrams and panel drawings.
The 13 checks every panel passes, plus witnessed FAT and SAT on site.
Controllers, I/O, networks and power, built to UL 508A and tested point by point.
Share your control narrative or describe the process. We will quote the programming together with the panel, or on its own.